Upward Momentum In Apparel Engineering
Our young, focused team manages the entire garment journey to meet the strict international requirements of global private labels.
Our End-to-End Manufacturing Journey
Material Sourcing
We source responsibly from certified suppliers, selecting materials that meet performance, comfort, and sustainability requirements.
Knit & Dye
Our knitting covers wide structures, while dyeing is handled by computerized labs and airflow systems for shade accuracy.
Detailing
Automated printing and embroidery systems deliver vibrant results and clean placement to strengthen the brand story.
Precision Cutting
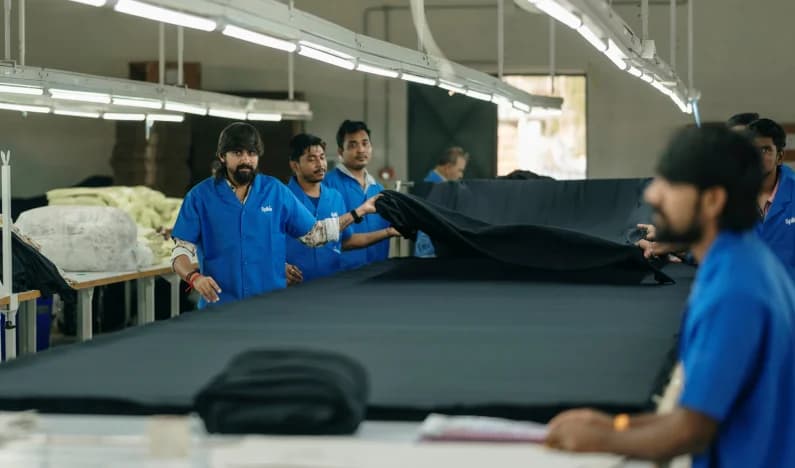
Fabrics are relaxed for dimensional accuracy, and markers are planned with high material efficiency.
Stitched Mastery
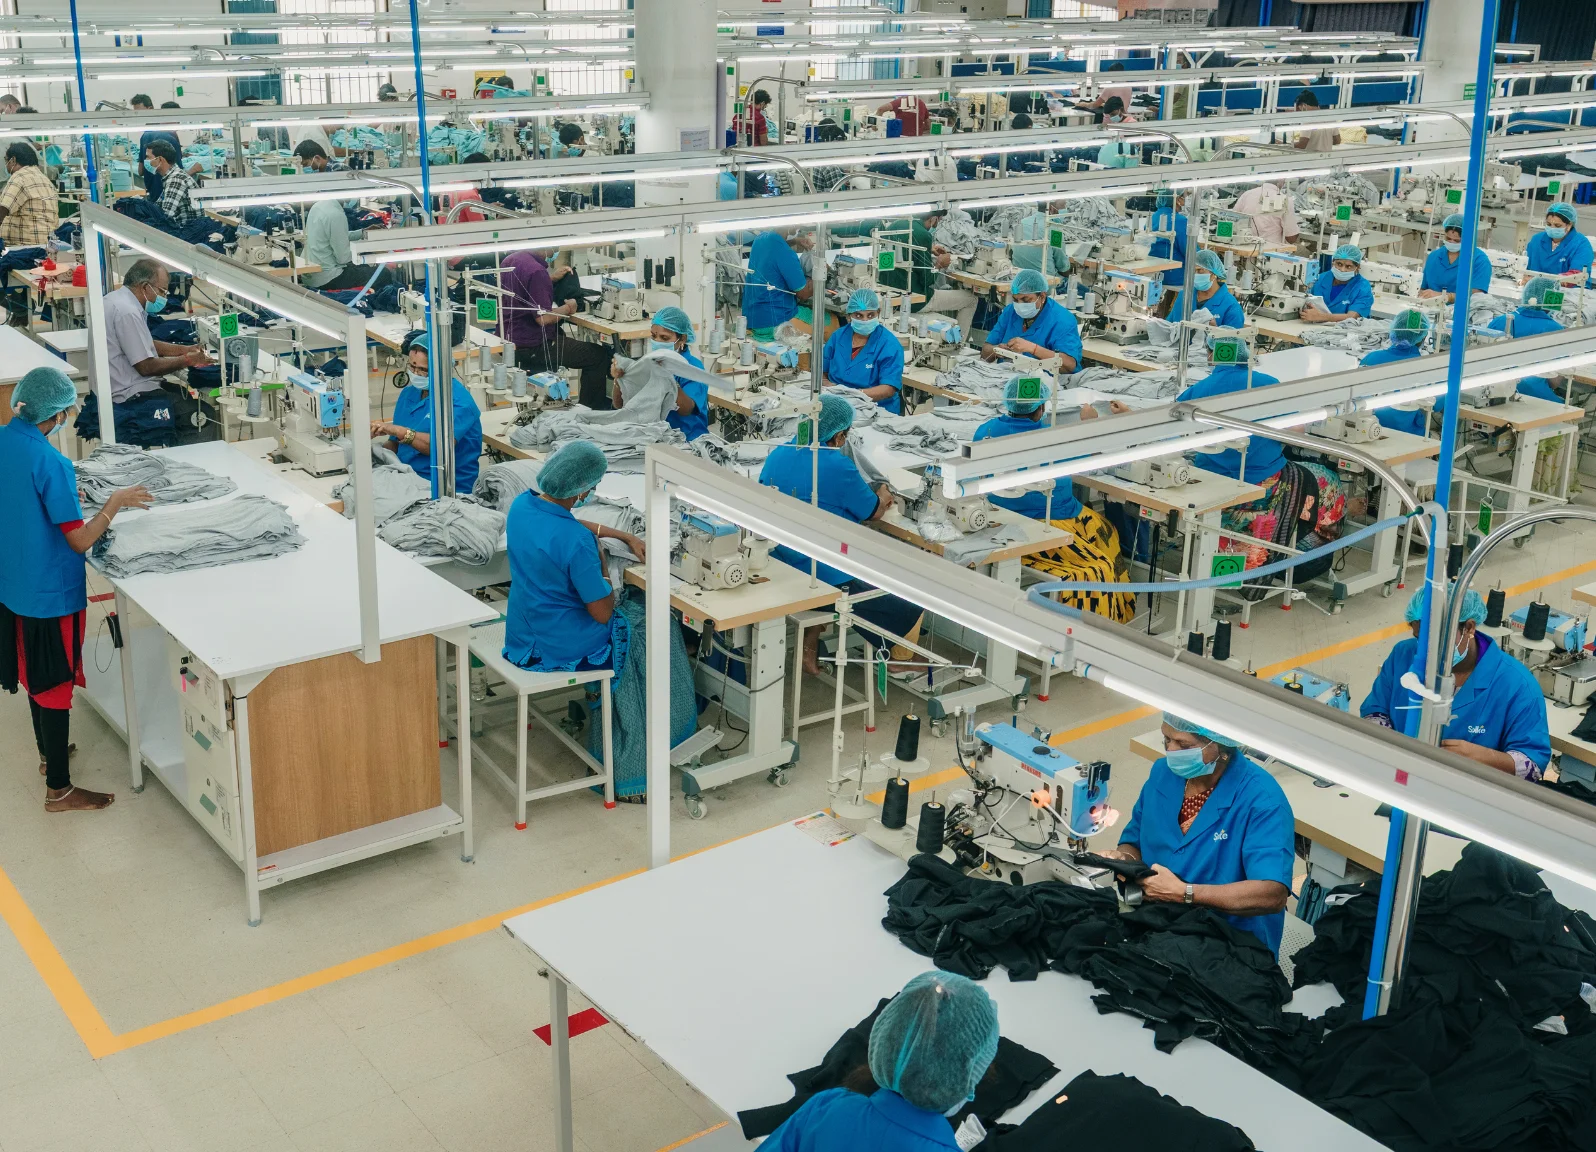
Skilled teams and balanced sewing lines manage every stage with specialized hosiery mastery and technical precision.
Rigid Inspections
Quality is built in through fabric testing, in-line inspections, and final AQL-based evaluations.
Final Processing
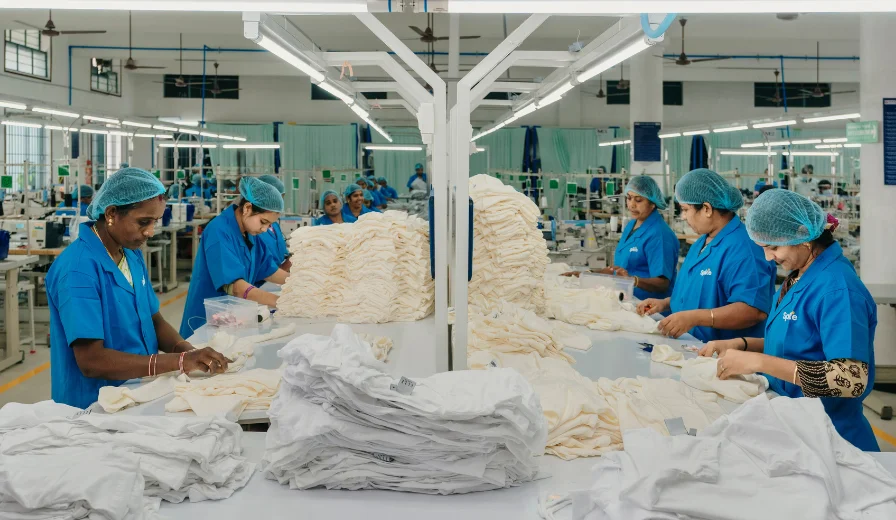
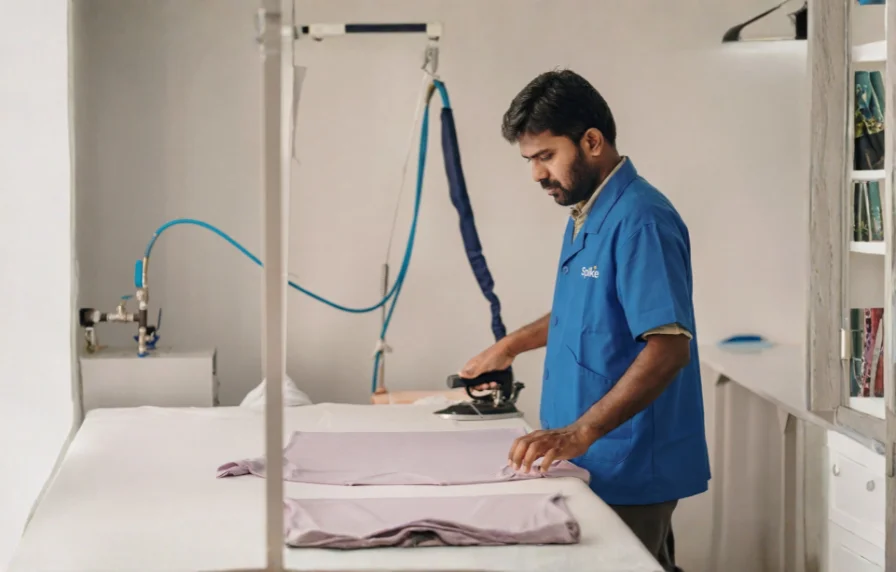
Every piece is steamed, shaped, and packed according to buyer-specific requirements for a professional finish.
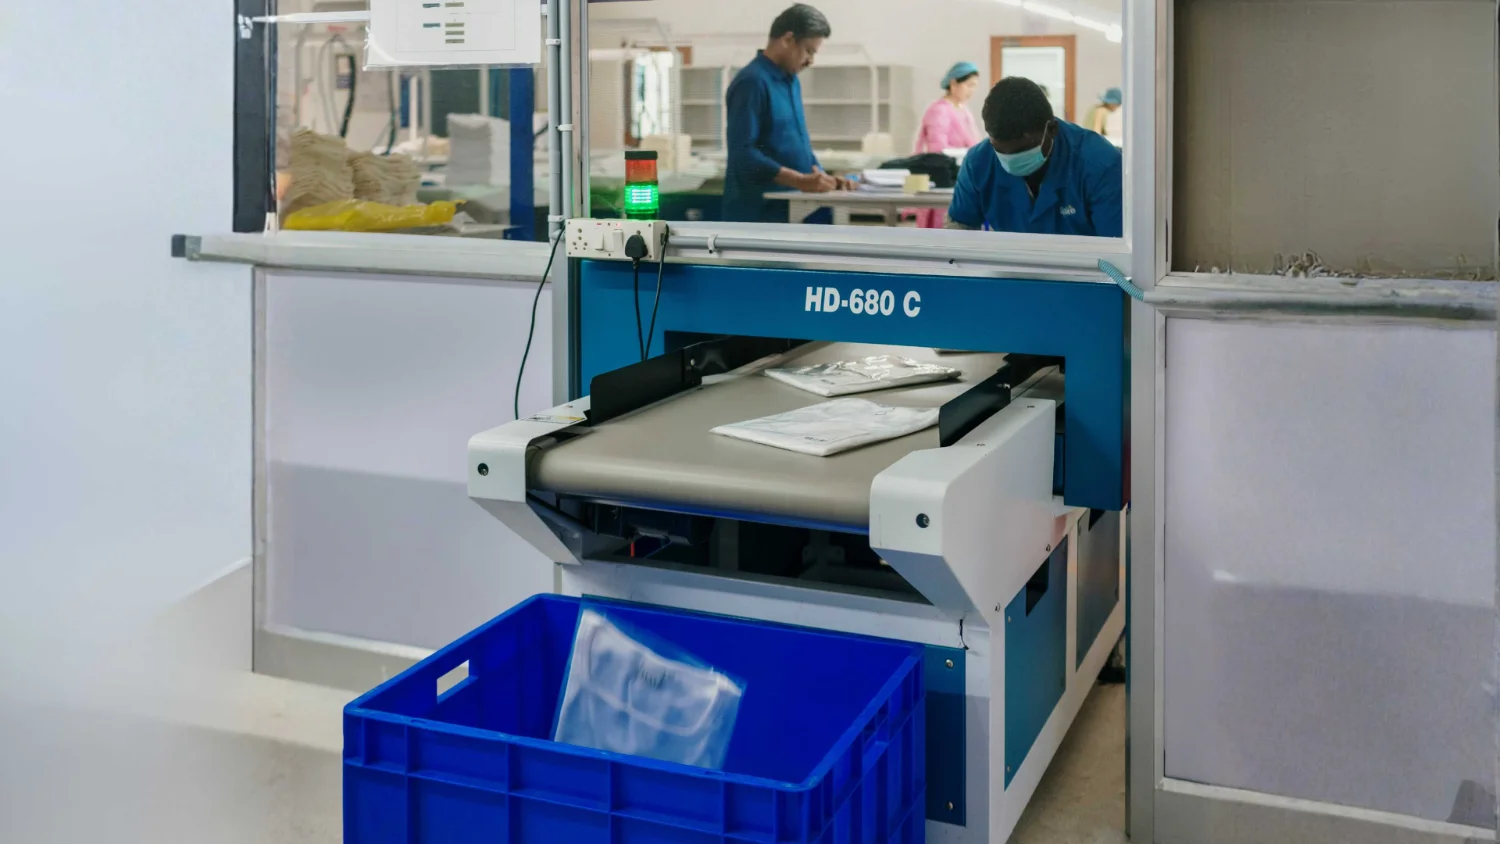
Secure Dispatch
Metal detection and barcoding ensure safety and traceability before orders are dispatched to global markets.
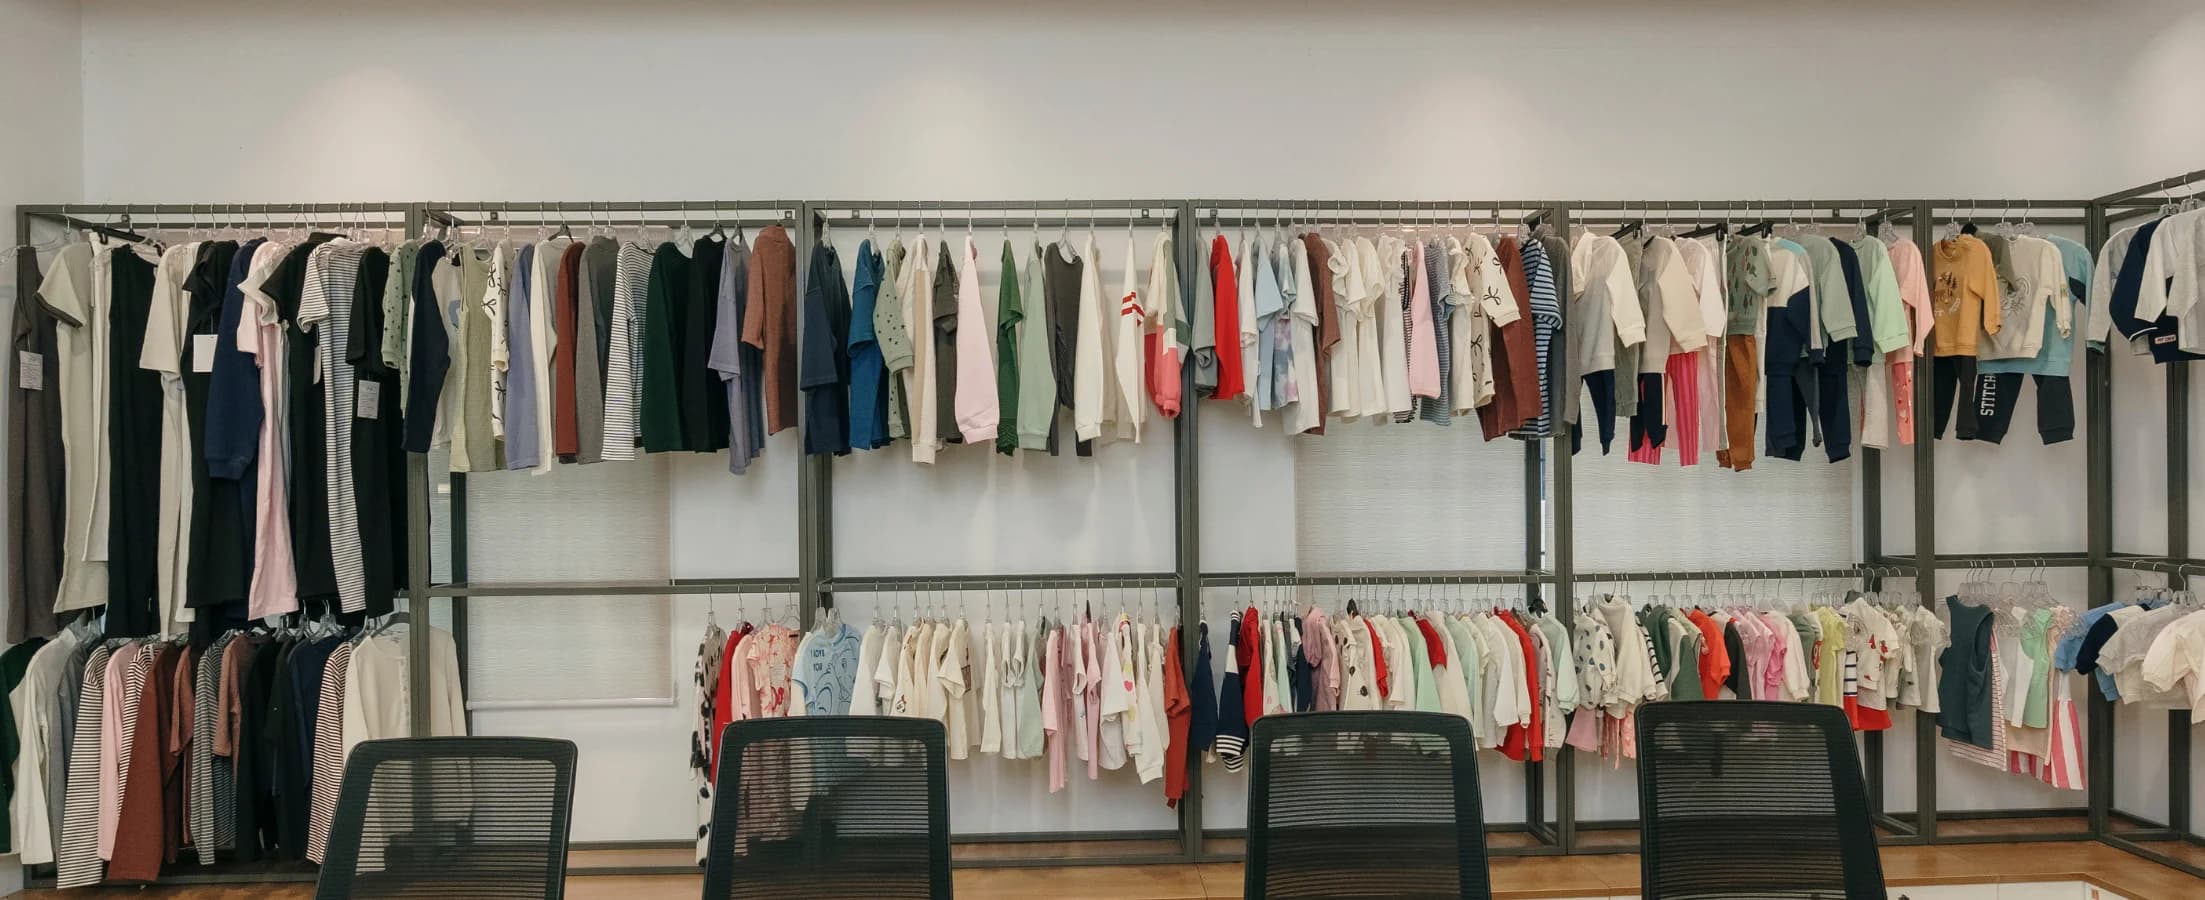

Scaling Quality Across Three Production Units
Our specialized textile infrastructure manages the entire manufacturing journey from our sampling lab to final export.
Dedicated teams provide proper service through meticulous in-line and final garment inspections.
Our manufacturing aligns with AQL standards and specific buyer quality manuals.
We honor our heritage by verifying all materials through testing at approved professional labs.
Every single stitch at critical operations is reviewed through 100% in-line checks.
Ensuring zero-compromise quality from start to finish.
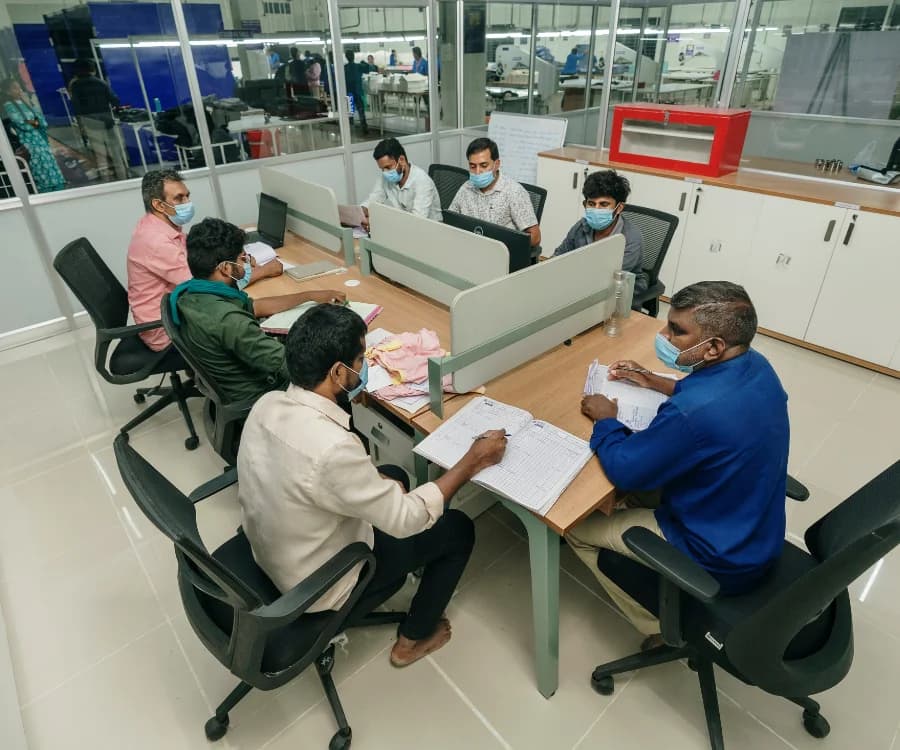
Operational Excellence
We ensure precision at every stage through dedicated QA teams, critical-operation checks, and AQL-standard compliance. With strong T&A planning, WIP tracking, early risk identification, and regular third-party audits, we deliver responsibly made products under safe and ethical working conditions.
Managing The Garment Journey At Capacity
Our facility is designed to manage every stage of production from our sampling lab to final export.
Manufacturing Power
Operational Capacity
Daily Capacity
Monthly Output
Scalable operations designed for both small batches and large-volume orders.
A Look Inside Our Specialized Facilities
From our computerized color labs to our high-bench capacity, discover how every aspect of our facility supports high-quality garment manufacturing.
Frequently Asked Questions
What is the best way to start working with Spike Creations?
What timelines can we expect across sampling and production stages?
How does Spike Creations ensure reliable and consistent delivery?
What results have you delivered for international clients?
Which global markets do you currently serve?
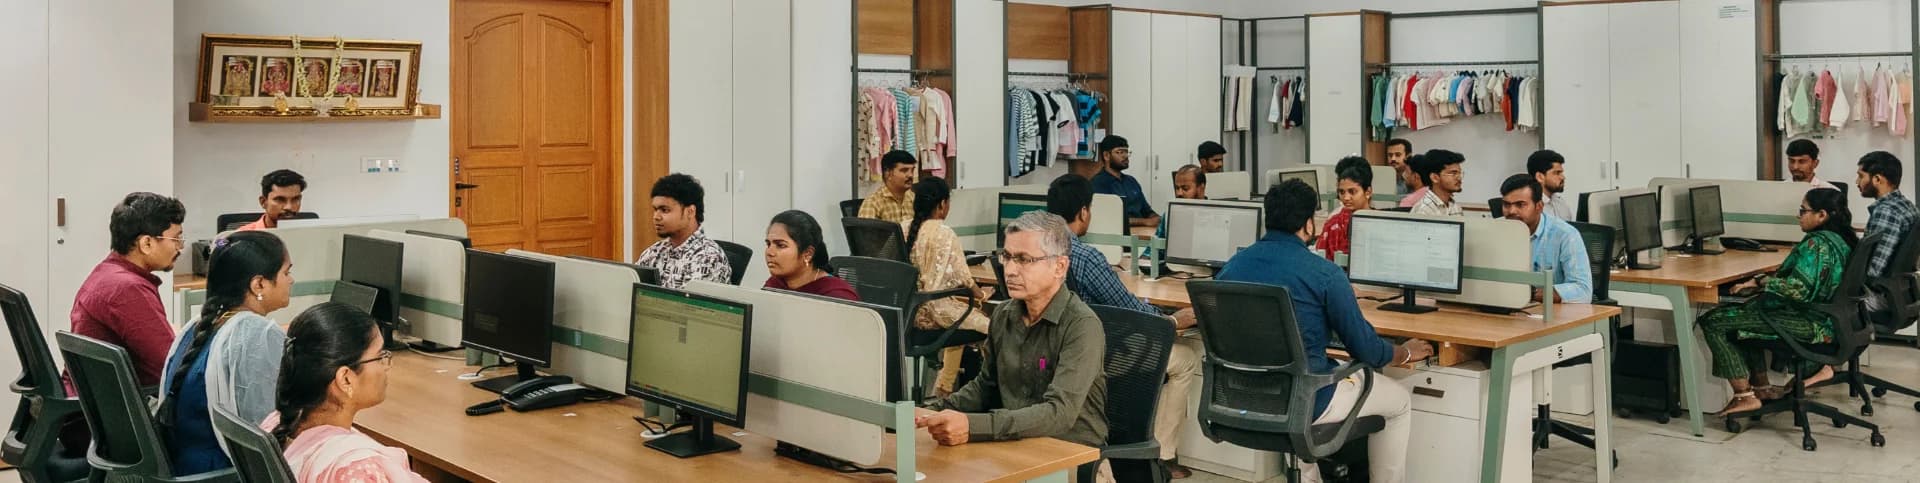
Do You Want To Scale Your Collection To Global Volumes?
Our high-capacity production units and specialized garment infrastructure can help you serve your international markets across the continents.